A supplier may promise “1,000 hours of salt spray resistance,” but what does that mean for a coated component installed outdoors in Ontario? Before choosing a finish or accepting a test report, manufacturers need to understand the exposure method, specimen preparation and acceptance criteria behind that number.
Salt spray testing and cyclic corrosion testing help evaluate metals and protective coatings under controlled laboratory conditions. They answer different questions, however, and neither automatically predicts how many years a product will last. This guide explains how to choose a useful corrosion test and connect the results with practical coating analysis, supplier qualification and product development.
Why corrosion testing matters for Ontario manufacturers
Consider an outdoor equipment bracket, painted enclosure or galvanized fastener. The purchasing question is usually practical: will the selected material and finish remain suitable for the intended environment? A laboratory program can provide comparative evidence before a large production order, or help investigate why an approved finish failed prematurely.
Coating durability remains an active industry concern. AMPP’s July 2026 corrosion and coatings update highlights surface preparation, application errors and environmental exposure among common contributors to coating failures. Testing should therefore examine the complete system: substrate, preparation, coating and intended service conditions. Looking only at the final paint colour or a supplier’s headline exposure time can overlook important differences.
What ASTM B117 salt spray testing tells you
ASTM B117 describes operation of a controlled salt-fog environment for evaluating the relative corrosion resistance of metals and coated metals. It provides an exposure practice rather than a complete product specification. The applicable customer or product requirement must establish the exposure duration, specimen details and interpretation of results.
This distinction matters when requesting a quotation. “Test to B117” does not by itself tell the laboratory whether a component should pass after 240, 500 or 1,000 hours, or which visible changes are acceptable. Specify the required edition and the purchasing document that defines acceptance. B117 results alone should not be converted into a predicted outdoor lifespan.
How cyclic corrosion testing differs
Cyclic corrosion testing changes exposure conditions according to a defined sequence. Depending on the method, specimens may experience fog, drying, humidity or other prescribed stages. The selected cycle, rather than the generic word “cyclic,” determines what the test actually does.
ASTM G85 covers five modifications of salt-fog testing. Some are cyclic, while Annex A1 is continuous. Annex A5, for example, uses a dilute electrolyte with alternating fog and drying. A request for “G85 testing” should identify the annex, exposure length and evaluation requirements. Different annexes are not interchangeable, and an OEM specification may call for a different corrosion method entirely.
ASTM B117
Continuous salt fog
Controlled exposure for specified corrosion comparisons.
ASTM G85 Annex A5
Fog → Dry → Repeat
A defined cyclic exposure using dilute electrolyte.
Method + duration + acceptance criteria make a test request meaningful.
Which corrosion test should you choose?
Start with the drawing, customer specification or purchase order. If it explicitly requires one method, substituting another without approval can leave you with a technically interesting report that does not satisfy the contract. Ask for clarification when the standard designation, edition or required endpoint is missing.
For product development, first define the decision: compare two pretreatments, screen coating suppliers, evaluate a design change or reproduce a known service problem. Select the exposure and measurements around that decision. A more complicated cycle is not automatically more useful; relevance depends on the material, environment and available validation.
Use a practical comparison plan. Keep the substrate and specimen geometry consistent, document the coating process, and include a reference finish where possible. Change one major variable at a time. Otherwise, an apparent improvement could come from a thicker coating or different preparation rather than the formulation being evaluated.
Prepare representative samples before exposure
Specimen preparation deserves as much attention as chamber time. A flat laboratory panel can help compare coating processes, but it may not represent a component with welds, threads, drainage pockets or cut edges. Decide whether panels, finished parts or both are needed before arranging the test.
Record each sample’s material, finish, batch and condition. Photograph the surfaces before exposure and distinguish existing damage from changes that appear later. Agree on which areas will be evaluated and how handling marks, contact points or intentionally protected surfaces will be treated.
For painted specimens, specify whether an intentional scribe is required. A scribe creates a controlled coating defect; an unscribed specimen answers a different question. Define its geometry and location under the applicable specification. Edge treatment also needs agreement, because exposed cut edges may influence the appearance of an otherwise intact coating.
Use repeat specimens where the decision warrants them. One part can reveal a problem, but it offers little information about variation between batches or individual components. Ask the laboratory to recommend sample quantities and dimensions for the selected method, available chamber space and reporting objective.
01
Define
Application, specification and decision.
02
Prepare
Samples, identification and baseline records.
03
Expose
Agreed method, duration and observations.
04
Evaluate
Document changes and compare with criteria.
A useful report connects the observations to the original purchasing or engineering question.
Read corrosion results beyond the hour count
A report should make clear what was exposed, for how long and how deterioration was assessed. Depending on the product and specification, observations may address substrate rust, coating blistering, corrosion around a scribe, disbondment or changes at edges. These are distinct outcomes and should not be collapsed into one vague “corrosion resistance” rating.
ASTM D1654 provides a framework for evaluating painted or coated specimens after corrosive exposure. Where specified and applicable, such evaluation helps compare the performance of the coating, pretreatment and substrate system. The exposure method and the evaluation method should both appear in the test plan.
For zinc-coated steel, clarify whether the requirement concerns white corrosion products associated with the zinc coating, red rust associated with the steel substrate, or both. Define the permitted location and extent of each observation. Photographs with consistent lighting and sample identification help reviewers understand the recorded condition.
A pass or fail statement needs an agreed limit. If no acceptance criterion was supplied, the appropriate output may be a documented set of observations rather than a blanket compliance claim.
Combine corrosion exposure with coating measurements
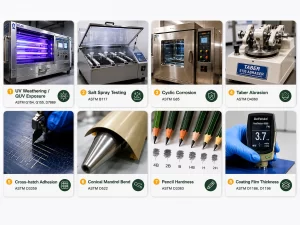
Exposure results become easier to interpret when the starting condition is known. Coating thickness measurements help establish whether comparison samples actually received similar finishes. ASTM D7091 addresses applicable nondestructive dry-film thickness measurement; instrument selection and measurement procedure must suit the coating and substrate.
ASTM D3359 adhesion ratings can provide additional information for suitable coating systems, but tape testing is not a universal measurement of bond strength. The method, film thickness and substrate should be considered when interpreting the rating. Post-exposure testing also requires an agreed recovery or conditioning procedure.
When a coating has already failed in service, failure analysis may be more informative than simply repeating a chamber exposure. Microscopy, cross-sectional examination and targeted chemical analysis can help investigate defects, contamination or material differences. The investigation should follow the evidence rather than assume the coating formulation is responsible.
What to send when requesting corrosion testing in Mississauga
A clear enquiry saves time and reduces assumptions. Include the material and coating description, sample quantity, approximate dimensions, required standard and edition, exposure duration, evaluation criteria and reporting deadline. Attach the relevant drawing or customer specification and identify any requirements for scribing, edge protection or interim photographs.
CMH Metlabs lists ASTM B117 and ASTM G85 among its ASTM testing services, alongside supporting coating and materials evaluations. Discuss the specific annex, specimen configuration and scope before shipping samples. To arrange a suitable program, request a corrosion testing quotation with your project details.
Frequently asked questions
1. How many hours of salt spray testing do I need?
The required duration should come from the customer specification or an agreed development plan. There is no single exposure time suitable for every coating or product. State what condition will be evaluated at the endpoint, so the chosen duration supports a clear decision.
2. Is cyclic corrosion testing better than ASTM B117?
It depends on the purpose. Follow the specified method for contractual testing. For development, choose a method relevant to the expected deterioration and available supporting evidence. A cyclic exposure is not automatically a better predictor for every material or application.
3. Can a salt spray result predict years of outdoor service?
There is no universal conversion from chamber hours to outdoor years. Service conditions and material behaviour vary. Treat the result as evidence within a defined test program, and use application-specific field data when making durability claims.
4. Should I send coated panels or finished components?
Panels can support controlled process comparisons; finished components can reveal geometry-related vulnerabilities. The right choice depends on the qualification requirement and engineering question. Confirm sample dimensions, preparation and quantities with the laboratory before cutting or modifying production parts.
5. What if the coating passes testing but fails in use?
Review whether the test represented the actual material, preparation and exposure. Preserve failed and unaffected samples, photographs and production records. A root cause investigation can assess the mismatch and guide corrective action instead of relying on the original pass result.