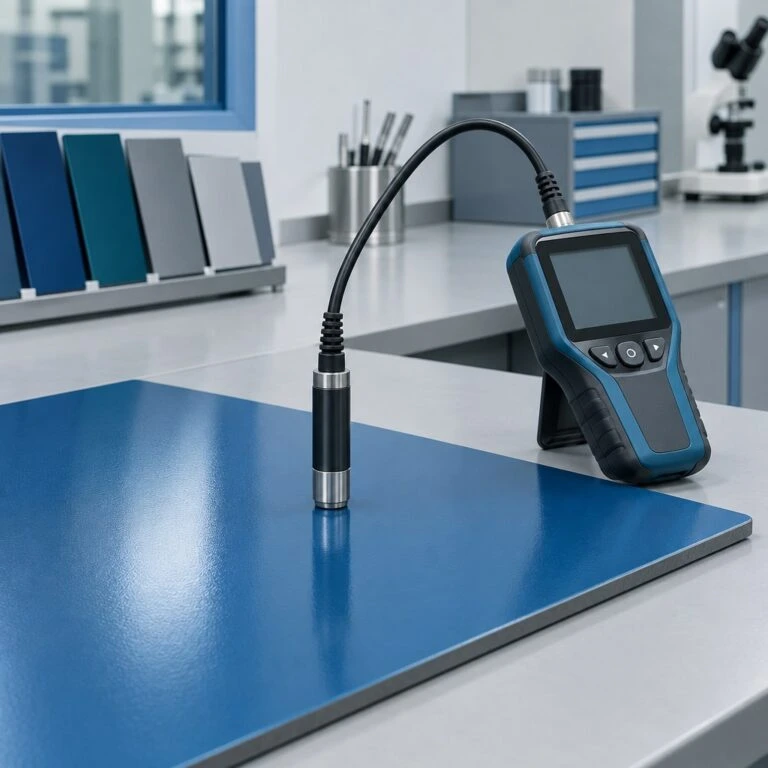
Coating thickness testing in Ontario helps fabricators, finishers and asset owners check whether a protective finish matches the specified build. A surface can look uniform while still requiring a documented thickness assessment. The useful result is a set of measurements tied to identifiable locations, an appropriate method and the correct acceptance criteria.
CMH Metlabs offers paint and coating thickness measurement for industrial enquiries in Mississauga and across Canada. This guide explains dry film thickness, the role of ASTM D7091, common measurement pitfalls and what to provide when arranging an inspection.
What is dry film thickness?
Dry film thickness, usually shortened to DFT, describes the thickness of an applied coating after it has dried. It differs from wet film thickness measured during application. Confirm which condition your specification requires before comparing results from different stages of a coating process.
Coating manufacturers specify thickness ranges for their products and systems. A thickness result should be reviewed against the applicable project documents and product information. More coating is not automatically an improvement: the intended range is part of the coating system’s application requirements. Thickness is one quality characteristic, rather than a complete demonstration of coating performance.
What does ASTM D7091 cover?
ASTM D7091 addresses magnetic and eddy current gauges for measuring dry coating thickness on suitable metal substrates. Its scope includes nonmagnetic coatings on ferrous metals and nonmagnetic, nonconductive coatings on nonferrous metals. It supplements the gauge manufacturer’s operating instructions.
The practice addresses calibration, verification and adjustment, along with measurement and reporting considerations. It does not provide one universal acceptable thickness for every paint system. Obtain the required limits from the governing specification and applicable coating documentation. Agree any required sampling or conformity procedure before inspection.
Do not assume a D7091 measurement plan applies unchanged to wood, concrete or plastic. Those substrates need a different technical approach. Similarly, identify any metallic intermediate layer before selecting a gauge: the complete coating and substrate combination matters.
Magnetic measurement may be suitable.
Eddy current measurement may be suitable.
Confirm what the probe measures and whether another technique is needed.
Method selection depends on the actual materials, geometry and measurement objective.
Three checks that make a gauge result meaningful
Calibration, verification and adjustment serve different purposes. Calibration is a documented assessment against traceable standards. Verification checks the instrument’s performance using suitable references in the intended measurement range. Adjustment adapts the gauge response to the measurement conditions where required by the instrument instructions.
A calibration certificate does not remove the need for checks during use. If readings appear inconsistent, the operator should investigate the instrument and application conditions before treating the displayed value as a material problem. Reference standards and the gauge both have tolerances that matter when reviewing a check.
For a purchase enquiry, ask how instrument identification and relevant checks will be documented. You do not need to prescribe a particular gauge brand. You do need confidence that the selected instrument is appropriate for the work and that its measurement basis can be explained.
Why surface profile and component shape matter
Surface roughness, curvature, proximity to edges, substrate composition and thin base metal can influence readings. A setup that works on a flat reference plate may need adjustment or a different probe for the actual part. Manufacturer instructions guide how those effects are addressed.
Provide information about blast preparation and the component geometry at quotation stage. Photographs should show the surfaces that need measurement, including narrow regions and curved areas. If an uncoated representative piece is available, tell the inspector; suitable substrate references can assist the setup.
Keep measurement access separate from coating condition. An inaccessible surface cannot be represented simply by measuring a convenient nearby face. Mark areas that cannot be reached and agree how they will be handled in the report. This makes the limits of the examination visible to the person approving the work.
Does the gauge measure each coating layer?
A conventional magnetic gauge on painted galvanized steel can respond to the combined paint and zinc thickness above the steel. That result should not automatically be labelled as paint-only thickness. Specialized instruments can separate particular duplex systems, but their suitability must be confirmed.
For primer, intermediate coat and topcoat systems, clarify whether you need individual coat thicknesses or the completed system total. Measurements recorded between application stages can help document layer build. A final reading alone may not separate the contributions of layers already applied.
CMH’s coating analysis services include cross-sectional analysis. If individual layers need examination, discuss whether a prepared section would address the question and whether cutting is permitted. Avoid assuming that every layer can be resolved nondestructively on every coating system.
Keep micrometres and mils consistent
Thickness is commonly reported in micrometres, written as µm, or mils. One mil is one thousandth of an inch, equal to 25.4 µm. A mil is not a millimetre. Check the report units before comparing a result with a drawing or supplier data sheet.
One thousandth of an inch.
Multiply mils by 25.4.
Divide micrometres by 25.4 to obtain mils.
Exact unit conversions only. These values are not measured results or recommended acceptance limits.
Plan an inspection that answers the project question
Start with the decision the inspection must support. Checking a supplied batch, investigating an uneven finish and accepting a coated structure are different tasks. Identify the relevant documents, then agree the examination coverage and reporting format with the laboratory.
- Identify the system. State the substrate, coating product names, number of coats and known intermediate metallic layers.
- Define the coverage. List component quantities, surfaces and locations requiring measurement, including any restricted access.
- Supply the criteria. Provide the required thickness range, document revision and any specified sampling or acceptance procedure.
- Confirm the condition. Explain whether the coating is newly applied, in service, repaired or awaiting another coat.
- Agree the deliverable. Request location references, recorded values, units and the required comparison with your criteria.
This checklist supports preparation; it is not a substitute for the sampling rules in a governing specification. If the request only says “test to ASTM D7091,” clarify the inspection coverage and acceptance basis before work begins. That prevents an avoidable disagreement over what the results demonstrate.
Read the report beyond the average
A useful report connects the component identity, measurement locations and results. Ask whether individual readings and grouped summaries will be retained. A broad average can make it difficult to see where a local variation occurred, especially when several different surfaces are combined.
Check that the reported thickness describes the intended layer or total system. Review stated limitations, inaccessible areas and any departure from the agreed plan. Where a conformity statement is requested, ensure the report identifies the acceptance document and the basis used for that statement.
If a result falls outside the requirement, preserve its location reference and discuss the next step with the responsible project team. The response may involve confirming the measurement, defining the affected area or reviewing the coating records. Repeatedly measuring different convenient points until an acceptable value appears does not resolve the original finding.
Thickness, adhesion and corrosion answer different questions
A coating can meet a thickness requirement while other properties still need evaluation. Thickness measurement does not directly measure adhesion strength or establish a service life. Select additional tests according to the product requirement or investigation objective rather than treating one result as proof of every performance characteristic.
CMH’s guide to coating adhesion testing explains the distinction between tape and pull-off approaches. Its article on salt spray and cyclic corrosion testing addresses a separate durability question. These methods can complement a coating assessment when their purpose and conditions are clearly defined.
Arrange coating thickness testing in Mississauga
To request a quotation, send photographs, component dimensions and quantities, substrate details, coating information and the relevant specification. State whether you need laboratory examination of submitted parts or a site inspection, and provide your location and requested completion date.
CMH Metlabs can review the enquiry and confirm the appropriate scope, access requirements and timing. A defined coating system, a clear inspection plan and an agreed acceptance basis make the final thickness report more useful for quality review and supplier discussions.